Design for Injection Moulding: 14 DFM Checks Before Tooling
Updated: 2026-10-20
Review wall sections, release direction, functional dimensions and assembly loads before committing to a mould. These 14 checks identify questions to resolve with the proposed manufacturer. They are a design checklist, not universal dimensional limits or evidence that a particular part will pass production testing.
What do coring and draft change in a part section?
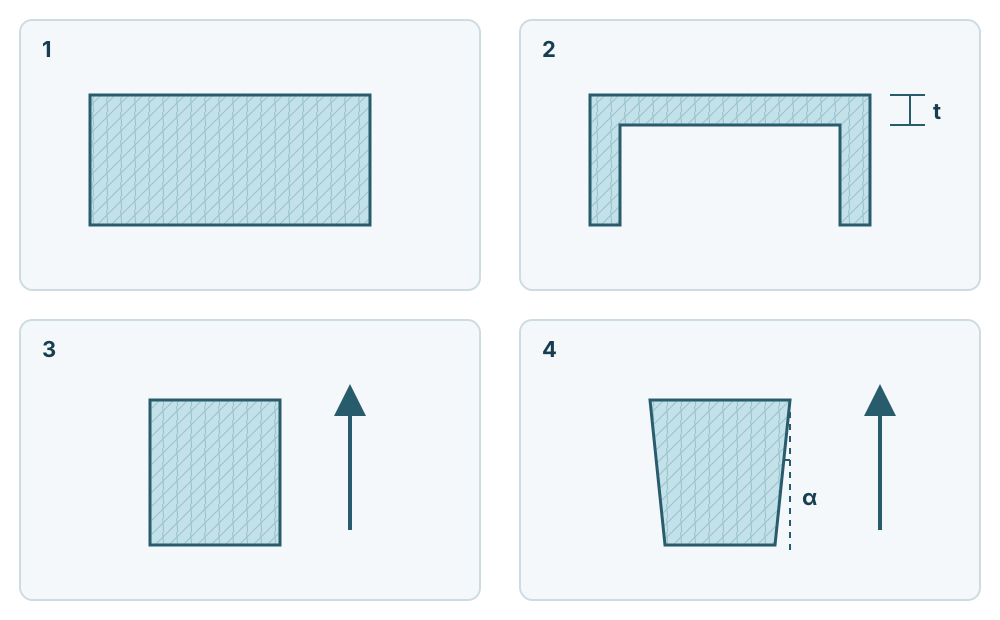
| Sketch | What to review |
|---|---|
| 1 → 2 | Coring removes a thick region. Review wall thickness t, stiffness and transitions together. |
| 3 → 4 | For the upward-opening cavity shown, draft α widens the feature towards the opening and helps release. |
Nordmould's schematic is an original teaching illustration, not a tested part or manufacturing drawing. It is not to scale. Radii, gates and ejectors are omitted. Set the actual wall and draft from the resin grade, depth, texture, function and proposed tool design; no angle or thickness is specified here.
Open the version 1 vector reference. For the engineering principles, see Protolabs' draft guidance and wall-thickness and coring explanation. These references do not validate a particular Nordmould production design.
What should the design review resolve?
1. Wall transitions
Use consistent sections where function permits. Review thick-to-thin transitions for uneven cooling, sink and warpage rather than applying a universal percentage limit.
2. Material and wall thickness
Choose the wall from the exact resin grade, flow length, load and process. ABS grades and part geometries do not share one guaranteed wall-thickness range. Ask the manufacturer to assess the proposed section.
3. Draft and release
Review every face along the intended opening direction. Set draft with the tool designer from depth, texture, shrinkage and release method; a single minimum angle does not fit every feature.
4. Ribs
Balance stiffness against filling, cooling and visible sink. Confirm rib thickness, height and root geometry together; a fixed ratio alone does not demonstrate a mouldable rib.
5. Bosses
Design screw and insert supports around assembly loads and the fastener specification. Avoid local masses and check cracking, sink and support ribs.
6. Undercuts
Mark features that prevent straight release. Compare redesign, side actions and inserts; any extra mechanism needs access, clearance and maintenance.
7. Parting line
Agree the split and witness-line position before freezing cosmetic or sealing faces. Review flash-sensitive areas and the direction of draft.
8. Gates and weld lines
Identify permitted gate marks and critical loaded or sealing regions. Review fill direction and weld-line risk; prediction is not a substitute for testing the required function.
9. Corners
Use radii that support load and flow without creating a thick junction. Set the actual radius from the local wall, material and mating geometry.
10. Coring
Consider a shell with ribs instead of a solid mass. Check the new section for stiffness, access and ejection; removing mass is not automatically an acceptable redesign.
11. Tolerances
Dimension functional interfaces and datums explicitly. Agree achievable limits, conditioning, measurement and inspection before ordering; no generic tolerance number establishes capability.
12. Snap fits
Calculate deflection, force and strain for the chosen grade, temperature and assembly cycles. Use grade-specific data and test the joint; do not apply a universal allowable strain.
13. Inserts
Provide insert drawings, positioning, thread and retention requirements. Distinguish moulded-in inserts from inserts installed afterwards and assess the relevant assembly loads.
14. Deep cores and holes
Assess core stiffness, cooling, venting and release. Depth-to-diameter feasibility depends on the tool; compare redesign or secondary machining rather than assuming a universal ratio.
Which numerical starting points can you check?
Protolabs publishes the following general wall-thickness guidance. Millimetres are converted from inches using 25.4 mm/in. These are screening ranges, not grade-specific limits or Nordmould specifications; assess flow length, loads and tool design before selecting a wall.
| Material | Source range, in. | Converted range, mm |
|---|---|---|
| ABS | 0.045–0.140 | 1.14–3.56 |
| PC | 0.040–0.150 | 1.02–3.81 |
| PP | 0.025–0.150 | 0.64–3.81 |
Protolabs describes 1–2° as a common draft starting point, with needs changing for depth, texture and release. Use its guidance to frame the review, not to approve a face without assessment. Protolabs
A geometry example, not a prescribed angle: for a 20 mm wall height and 1° draft, the lateral offset is 20 × tan(1°) ≈ 0.35 mm per side, or 0.70 mm across two opposing sides. Check whether that change affects fit and which plane defines the nominal dimension.
Which references and assumptions support these checks?
The checklist identifies geometry and acceptance decisions. Keep resin data, a sectioned CAD view, the release direction and a revision-controlled drawing with the DFM notes. Manufacturer references explain general principles, not approval of a Nordmould part.
Frequently asked questions
What is DFM in injection moulding?
DFM is a review of geometry and requirements before tooling. Nordmould offers a free written review; its scope and open questions should be agreed for the project.
How does unresolved design affect tool cost?
Unresolved geometry can require additional tool mechanisms, machining or revisions. The cost depends on the proposed change; this checklist does not estimate a universal euro penalty.
How should ABS wall thickness be selected?
Choose ABS wall thickness from the exact grade, flow length, function and tool proposal. Ask for assessment of the actual section; no single range is a guarantee for every ABS part.
How much draft does a moulded part need?
Draft depends on release direction, depth, texture, material and tool construction. Agree each critical face with the tool designer instead of treating one angle as a universal minimum.
Can a moulded part contain undercuts?
Undercuts may be possible through redesign, side actions or inserts. The proposed manufacturer must assess release, access, cost and maintenance for the actual feature.
Is there one maximum rib ratio?
There is no universal maximum rib ratio. Review rib height, thickness, root, filling and visible sink together for the selected material and proposed process.
Why does gate location matter?
Gate position affects filling, visible marks and possible weld-line locations. Agree permitted regions and assess critical loads or seals with appropriate review and testing.
Send the current STEP model and drawing to Nordmould for a free DFM review. Identify the critical functions, material grade, cosmetic zones and open decisions; agree the review scope and any simulation or testing separately.
DFM / RFQ
Injection Moulding Calculators & Selectors
Last reviewed: 2026-05